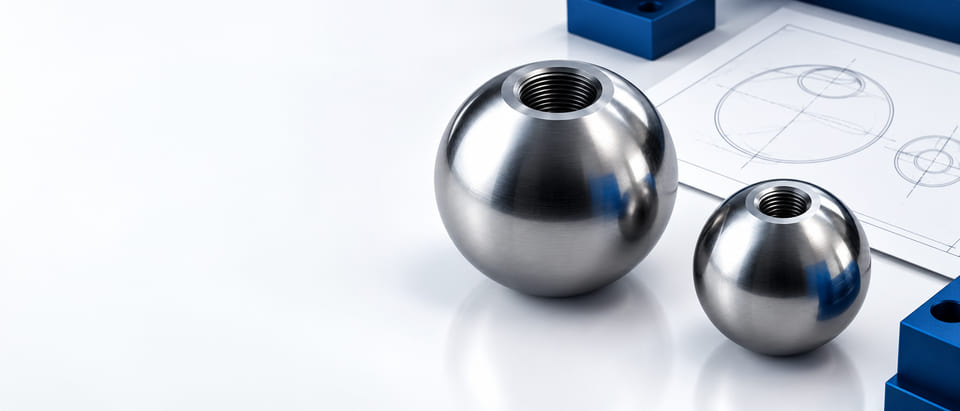
A sphere with a threaded hole is an interface, not simply a ball plus a thread size. This guide explains how to turn its geometry and mating relationship into a clear drawing, inspection plan and supplier enquiry.
Quick Answer: What Must a Threaded Ball Drawing Specify?
A threaded ball drawing must define the spherical geometry and the attachment feature together. State ball diameter and relevant tolerance, material and condition, thread designation, blind or through construction, required thread engagement, hole depth where applicable, and the relationship of the hole to the chosen datum. Surface and inspection requirements remain separate.
Do not assume that nominal thread size defines drilled depth, full-form thread length or usable engagement. Those dimensions can differ, especially in a blind hole. The mating fastener and load path determine what the assembly needs, while manufacturing feasibility and inspection establish whether the feature can be supplied as intended.
MEITUO's threaded-ball enquiry route is useful when a standard sphere description no longer captures the complete part. Share the mating component, drawing revision and function. This guide focuses on a clear attachment specification rather than prescribing universal engagement or tightening values for every ball and thread.
How Should a Spherical Part Be Located for the Attachment Requirement?
A sphere does not present the same obvious locating faces as a rectangular block. The drawing must establish a meaningful relationship between the exterior geometry, hole axis and any assembly feature that controls function. Merely adding the word concentric does not explain what is being evaluated or how the part is held.
Choose the datum scheme and geometric requirement with the component designer. The appropriate control depends on the function and the applicable drawing conventions. Avoid mixing geometric symbols from different conventions without identifying the governing basis. The supplier needs a requirement it can interpret and inspect.
Show how the hole relates to the intended mounting direction or contact area. A threaded handle, fixture locator and decorative attachment may need different control. Tightening every geometric feature can increase inspection and production effort without addressing the actual assembly requirement.
Where the design is still conceptual, provide an interface sketch and identify the critical relationship as an open engineering action. That is more useful than inserting a precise-looking tolerance without a functional reason. The review should end in a controlled drawing, not an informal agreement that the hole looks centered in a photograph.
What Is the Difference Between Hole Depth and Thread Engagement?
A blind drilled hole can contain an entry chamfer, a fully formed threaded region, incomplete thread near the end and the drill-point region. The exact details depend on the route. A single depth callout can therefore leave ambiguity about how much usable thread the assembly actually receives.
Specify the dimension that matters to the mating fastener. Required full-form thread length, total hole depth and usable assembly engagement should not be treated as identical by default. If the drawing must constrain more than one, state them distinctly and confirm the relevant inspection method.
The mating stud or screw has its own tolerances and end condition. A fastener can bottom in a blind hole before the joint reaches its intended seating condition. That problem may not be visible when the components are inspected separately. Evaluate the actual assembly and retain the controlling interface dimensions.
Do not choose engagement from a universal multiple quoted for another material or loading condition. Material strength, thread form, loading, vibration, temperature and the consequence of failure may affect the design. Engineering should establish the required connection; the supplier should confirm the proposed component and inspection scope.
State whether the attachment is an internal thread in the sphere or an external threaded feature attached to it. Specify the thread system, nominal designation, pitch or equivalent system detail, tolerance class where required and handedness if it is not the ordinary assumed direction. The phrase ISO thread is not enough to identify all those choices.
For a transparent pitch illustration, imagine a hypothetical single-start thread with pitch 1.25 mm. Four turns correspond geometrically to 5 mm of axial advance. That arithmetic does not prove 5 mm of usable load-bearing engagement: entry features, incomplete threads, seating and the actual mating positions still need review. It is an example of thread geometry, not a recommended connection.
If an external stud is part of the supplied component, define how it relates to the sphere and how its relevant attachment is accepted. A sphere with a tapped hole and a sphere with an attached stud are not automatically equivalent routes, even when the mating equipment uses the same nominal thread label.
Blind-Hole vs Through-Hole Threaded Balls: Which Details Change?
The construction decision affects more than whether an opening is visible on the opposite side. It can influence fastener clearance, drainage, appearance, cleaning and the remaining material around the feature. Use the comparison to expose the relevant questions, not to declare one construction universally stronger.
| Decision | Blind-hole route | Through-hole route |
|---|---|---|
| Depth | Distinguish total depth and usable thread | Define thread extent and exits |
| Fastener fit | Check bottoming and actual engagement | Check protrusion and clearance |
| Appearance | Specify intact exterior where required | Specify exit condition and edge finish |
| Cleaning | Consider retained fluid or debris | Consider flow path and cleanability |
| Inspection | Define accessible evidence | Define both entrance and exit acceptance |
If the hole must remain blind for appearance or function, show that requirement on the drawing. If the through route is acceptable, identify the effect of any protruding stud or exposed thread on the surrounding assembly. A supplier should not be left to select the construction because one process is more convenient.
Consider the installed orientation and environment. A feature that retains cleaning fluid or debris may need a different handling or inspection plan from an open attachment in dry service. Keep those requirements connected to the actual duty rather than adding a generic sealed or hygienic label.
How Can a Thread-Depth Stack Reveal a Bottoming Risk?
Consider a hypothetical blind-hole drawing with 12 mm of specified full-form thread and an assembly requiring 10 mm of intended engagement. Assume the drawing also defines sufficient total hole depth and appropriate end clearance. The numerical difference between those two specified thread lengths is 2 mm, but that arithmetic alone does not establish a safe connection or the correct clearance.
Now suppose the mating stud projects 13 mm beyond its seating face. That geometry creates a question that must be resolved against the actual hole and thread details. It cannot be approved merely because 13 is greater than the intended 10 mm engagement. The stud may interfere with an end region before the assembly seats as intended.
Record the controlling faces and feature definitions in the stack. Entry chamfers, unthreaded lengths, incomplete threads and seating features may affect the usable assembly. Treat this example as a drawing-review method, not a recommended hole or thread design.
Where a change is proposed, show the revised interface and approval scope. A successful fit with one convenient sample stud does not prove that the full permitted stud population will assemble correctly. The tolerance stack and relevant test should represent the actual components being purchased.
Which Surface and Edge Conditions Need Their Own Acceptance?
The sphere may serve as a visible handle, a contact surface or a locating component. Identify the areas where scratches, dents or finishing changes are critical. A general polish description should not leave the supplier to guess whether appearance or functional surface condition governs rejection.
Specify thread entry and exit conditions where they affect assembly or handling. Burrs, sharp edges and residual debris can create different problems from an incorrect thread size. Include appropriate cleaning and handling requirements without assuming that a bright exterior establishes a clean internal feature.
If a coating or plating is required, define how the finished exterior and threaded feature are controlled. Processing can affect dimensions and the mating fit. The drawing and quotation need to identify whether the thread requirement applies before or after the relevant finish and how masking or other details are handled if necessary.
Separate cosmetic samples from engineering acceptance. A retained appearance sample can help establish a viewing standard, but it does not establish thread geometry or connection performance. Conversely, a correctly gauged thread may still sit in an unacceptable external sphere. Both aspects must be reviewed for the component's intended use.
How Should a Buyer Inspect a Threaded Ball Without Overclaiming?
Assign an inspection method to each critical feature: exterior dimensions and form, thread requirement, depth, geometric relationship, surface and cleanliness. A single assembly check does not prove every feature, and a thread gauge does not establish all dimensions around a blind hole.
Use suitable gauges and procedures for the stated thread convention and acceptance. Define the evidence that will be retained and how it represents the supplied lot. If access limits the inspection of an internal feature, resolve the appropriate method during development rather than discovering the issue after production.
Functional tests should address the connection's actual duty. Do not use an arbitrary tightening value copied from another material as the acceptance for every threaded sphere. The designer must establish the relevant load and assembly conditions, while the supplier confirms what is included in its proposed test or inspection.
An inspection report should preserve the drawing revision, part identity, sample basis and results. If a first article establishes a new requirement, transfer that approved basis into the production order. Keep proposed deviations visible so a drawing discussion does not turn into an undocumented change between the sample and the recurring purchase.
A functional fit check should use the intended interface or an approved inspection representation. A convenient screw from a drawer can provide development feedback without representing every tolerance and end condition of the actual fastener population. Identify the reference used and the requirement it demonstrates.
Where the surface finish extends near the hole entry, define the transition and viewing or functional acceptance. An entry chamfer can be necessary for one feature but can also change the visible or contacting region of the sphere. The drawing should make the intended compromise clear rather than leaving it to cosmetic interpretation after production.
Record how a depth result is obtained. Full thread, total drilled depth and accessible probe depth can be different observations; a report should label the relevant one. If the feature cannot be checked adequately after a particular assembly or finish, agree the necessary process-stage evidence during development.
For a repeat part, keep the approved mating reference and gauge basis with its drawing. A later change to fastener length, coating or seating can affect the joint even though the ball drawing appears unchanged. Reviewing both sides of the interface prevents the threaded sphere from becoming the default explanation for every assembly problem.
Keep the first-article check connected to the eventual production fastener, including its permitted end and finish conditions. An attachment that assembles with one hand-selected mating part has not necessarily demonstrated the complete tolerance relationship.
How Should Threaded-Ball Buyers Compare Suppliers in China and India?
A threaded sphere is a drawing-controlled attachment component, so the useful market comparison concerns interface interpretation and evidence. China and India are included here as sourcing examples; this does not establish a common supply capability across all suppliers in either country.
Keep the same thread convention, controlling dimensions and assembly question in each enquiry. A familiar thread label should not conceal different hole construction or usable engagement.
China: a specification-led sourcing review
For China sourcing, MEITUO Balls in Qingdao can review a sphere-and-thread brief that includes the mating fastener. State whether the requirement is blind or through, identify the critical surface and attach the released drawing rather than quoting from a photograph.
Ask the proposed seller to identify its process and inspection scope where these affect qualification. If a depth or datum is unclear, resolve it before sample approval. Retain the accepted interface with the purchasing record so later orders do not revert to a generic ball-with-hole description.
India: compare the actual requirement
Dular Steel Products in Agra is an identifiable Indian supplier example for researching precision components and custom requirements. Confirm whether the specific threaded sphere is within its current offered scope; a broad custom-product statement is not proof of a finished attachment design.
When comparing an Indian proposal with MEITUO, retain the controlling thread standard, drawing revision and required usable engagement. Check how samples and reports identify blind-hole depth and the relationship to the sphere. Resolve any terminology differences before discussing nominal price, especially when a replacement is being sourced from an existing component without a complete drawing.
How Can MEITUO Help Turn a Threaded-Sphere Sketch Into a Purchase Brief?
MEITUO Balls is associated with Qingdao Meituo Steel Co., Ltd., Qingdao, China. A useful threaded-ball conversation begins with the complete attachment: sphere, hole, thread, mating part and the function the joint must support.
Provide the intended duty and explain what is already fixed by the design. If the main uncertainty is bottoming, share the fastener projection and relevant seating faces. If alignment or appearance is critical, show the interface and required surface. An existing sample can help communication, but its condition and missing requirements need to remain visible.
Use the threaded ball product route and custom development service to prepare the enquiry. Supply and process feasibility, sample basis, inspection and commercial terms require confirmation for the particular component.
MEITUO can be considered when the buyer needs those questions organized before quotation. This is not a claim that every thread, material or tolerance is already available, nor that a generic sample proves connection safety. The component owner should approve the defined interface and the relevant validation before series purchasing.
Threaded Ball Drawing Requirements FAQ: What Should Buyers Ask?
Does thread size define hole depth?
No. Specify the required thread and depth features separately, including usable engagement where it matters. Blind-hole end regions and entry features can affect the assembly.
Is a blind hole always preferable?
No. The function, appearance, cleaning and interface determine the construction. Identify whether blind or through is required instead of allowing an unstated choice.
Can a thread gauge prove the hole is centered?
No. Thread acceptance and its geometric relationship to the sphere are different requirements. Define an appropriate datum and inspection basis.
Does more stud projection guarantee better engagement?
No. Excess projection can create interference or bottoming. Review the actual interface and tolerances rather than a single length comparison.
Does a polished exterior prove a clean thread?
No. Internal debris and entry condition need suitable acceptance where relevant. Exterior appearance does not establish every internal feature.
What should a first threaded-ball enquiry contain?
Provide material, sphere geometry, thread requirement, blind/through construction, relevant depths, datums, mating fastener, duty, quantity and required inspection evidence.